
Electrical Cabinet Door Panel Manufacturing
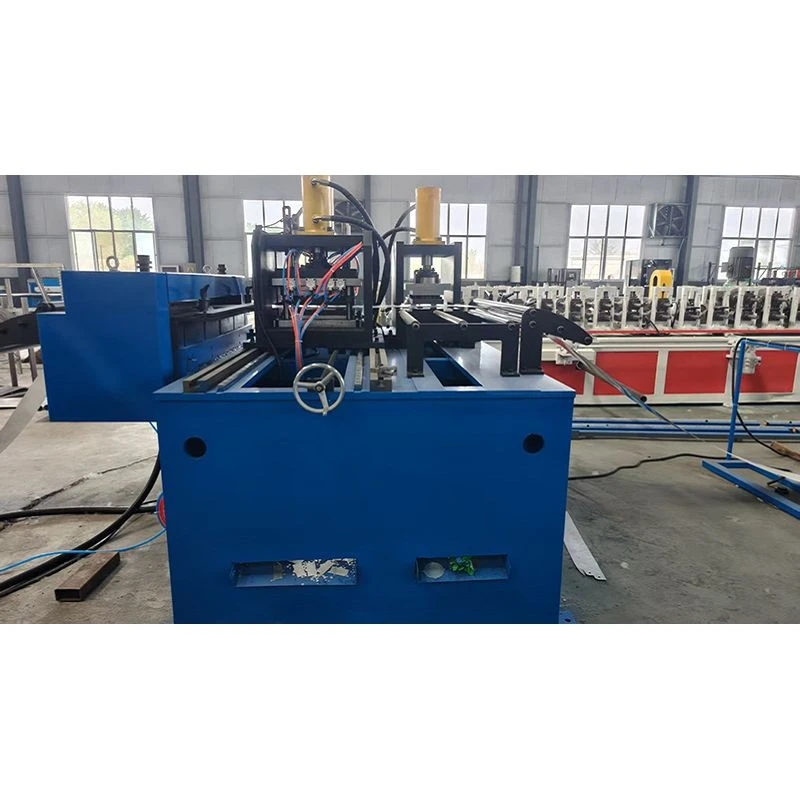
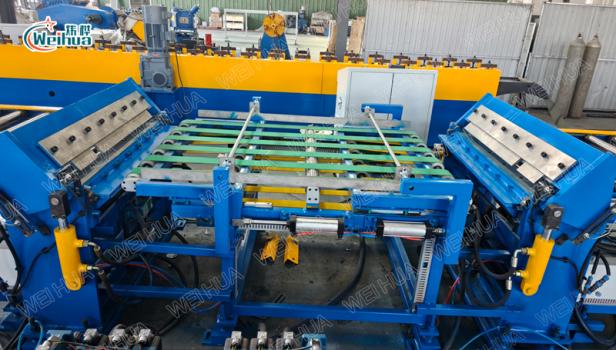
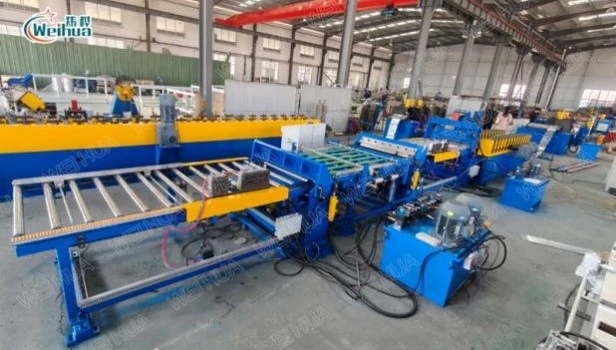
The electrical cabinet door panel manufacturing equipment is the core forming machine of the door panel production line, specifically designed to process steel strips into finished door panels through multiple rolling and bending processes. This equipment integrates feeding, punching, shearing, conveying, and bending, employing Cr12 hardened rollers (HRC58°-62°), PLC control, and variable frequency motor drive. Production speed is 0-4 pieces/minute, cutting accuracy is ≤±0.5mm (length ≤3000mm), total power is 30kW, and it can process plates with thicknesses of 0.5-1.5mm and widths of 100-1000mm, suitable for the automated manufacturing of various electrical cabinet door panels.
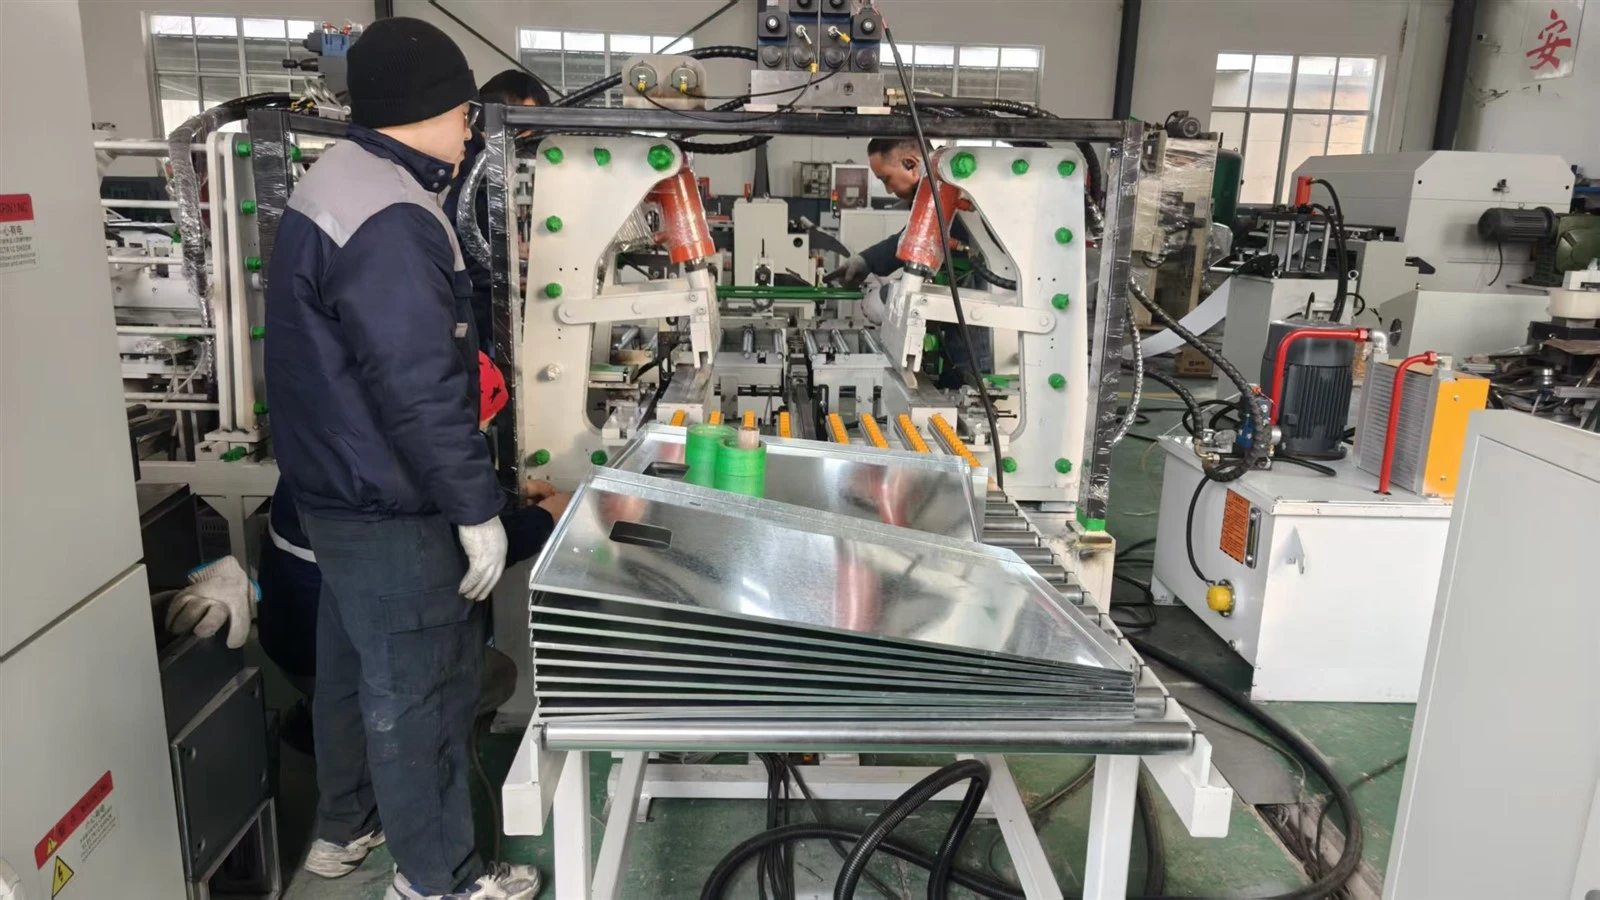
Technical Specifications
|
Product Name |
Electrical Cabinet Door Panel Manufacturing |
|
|
Material Specification |
Q235 |
|
|
Production Speed |
0-4pcs/min |
|
|
Cutting Method |
Shearing Machine |
|
|
Voltage Parameters |
380V/415V, 50Hz, 3-phase |
|
|
Electrical Control |
PLC |
|
|
Drive Motor |
Variable Frequency Motor Drive |
|
|
Strip Thickness |
0.5-1.5mm (Customized according to customer requirements) |
|
|
Strip Width |
100mm-1000mm |
|
|
Roll Material |
Cr12, Quenched HRC58°-62° |
|
|
Hydraulic Oil Type |
46# Hydraulic Oil |
|
|
Gear Oil Type |
18# Gear Oil |
|
|
Total Motor Power |
30KW |
|
|
Cutting Dimension Tolerance |
≤ ±0.5mm (Length ≤ 3000mm) |
|
|
Cutting Die Material |
Cr12MoV |
|
|
Air Source |
0.5m³/Min; Pressure: 0.7MPa |
|

Product Advantages
High-precision cutting with automatic conveying:
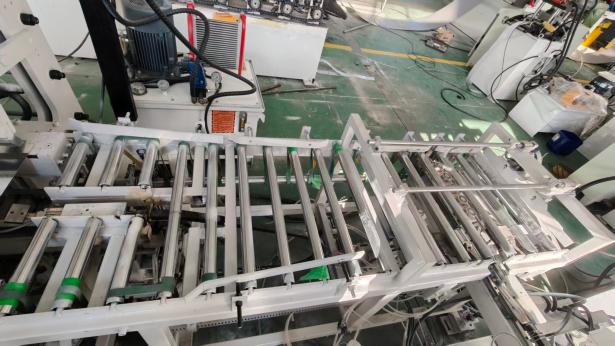
The equipment uses a shearing machine instead of hydraulic cutting, resulting in smooth, burr-free edges and dimensional tolerances controlled within ±0.5mm (length ≤3000mm). The cut door panel blanks are smoothly transferred to the bending station via an automatic conveyor platform, eliminating the need for manual handling and secondary positioning, preventing bumps and deformation during transport, and ensuring consistency between the bending and cutting references.
Multi-pass roll forming enhances door panel rigidity, preventing deformation of thin panels:
Large door panels with thin surfaces (minimum 0.5mm) are prone to deformation due to insufficient rigidity. Before bending, the equipment uses multiple progressive roll forming processes to integrally form a longitudinal reinforcing rib structure on the door panel surface, enhancing the panel's bending strength. The reinforcing ribs are integrally formed with the door panel without additional welding, maintaining a clean appearance and ensuring the door panel does not collapse or twist during long-term use.
Unified punching and bending references ensure good interchangeability of finished products:
All processes are completed continuously on the same equipment, with punching, cutting, and bending sharing the same feeding reference. During bending, the cut end face is used as the positioning reference. The relative relationship between the bending line and the punching position is guaranteed by the servo feeding system throughout the process. In mass production, the positions of all door panel hinge holes and lock holes are completely consistent with the distance of the bending edge, resulting in good interchangeability of finished products and no need for selection during assembly.
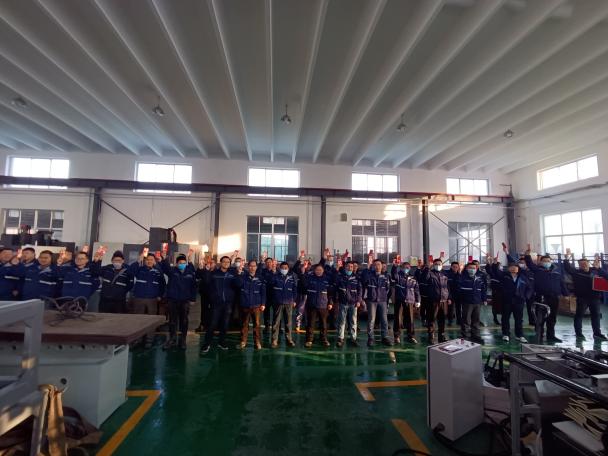
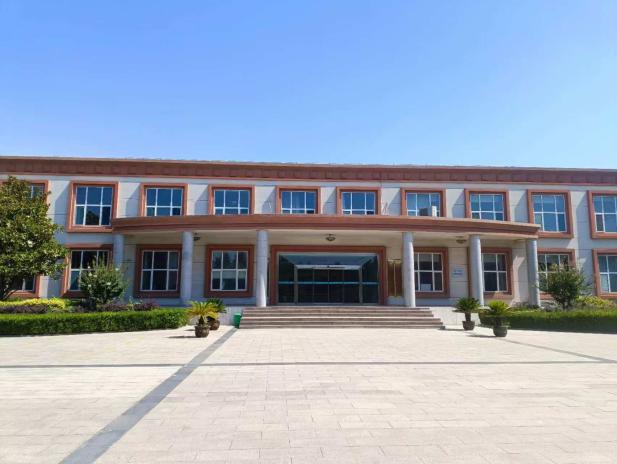
Factory photos
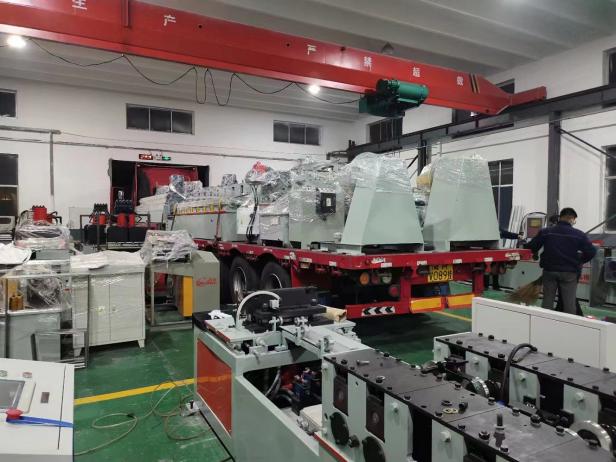
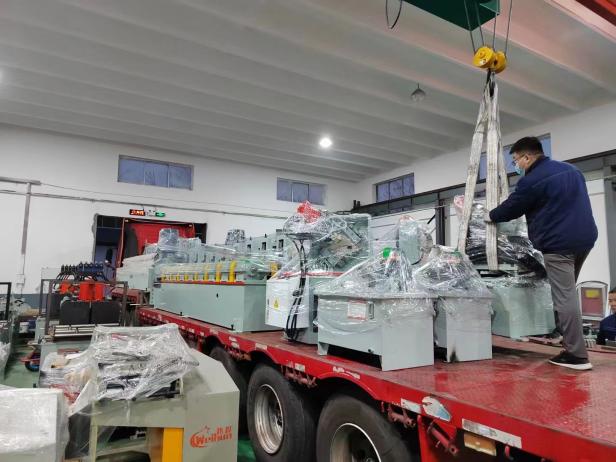
Shipping photos
Customer visit
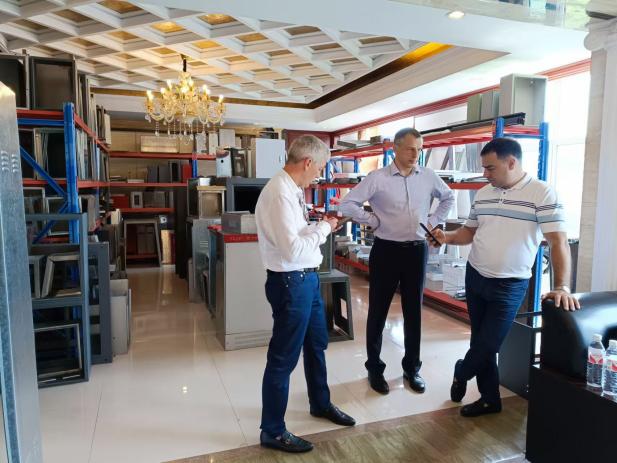
FAQ
Q: Are you a factory or a trading company?
A: We are a factory located in Weifang, China. It possesses over twenty sets of advanced equipment, including a new precision machining center, NC lathes, CNC wire EDM machines, and a large automotive profile bending test platform. You are welcome to visit our factory at any time.
Q: What are the differences between this equipment and other equipment in the door panel production line?
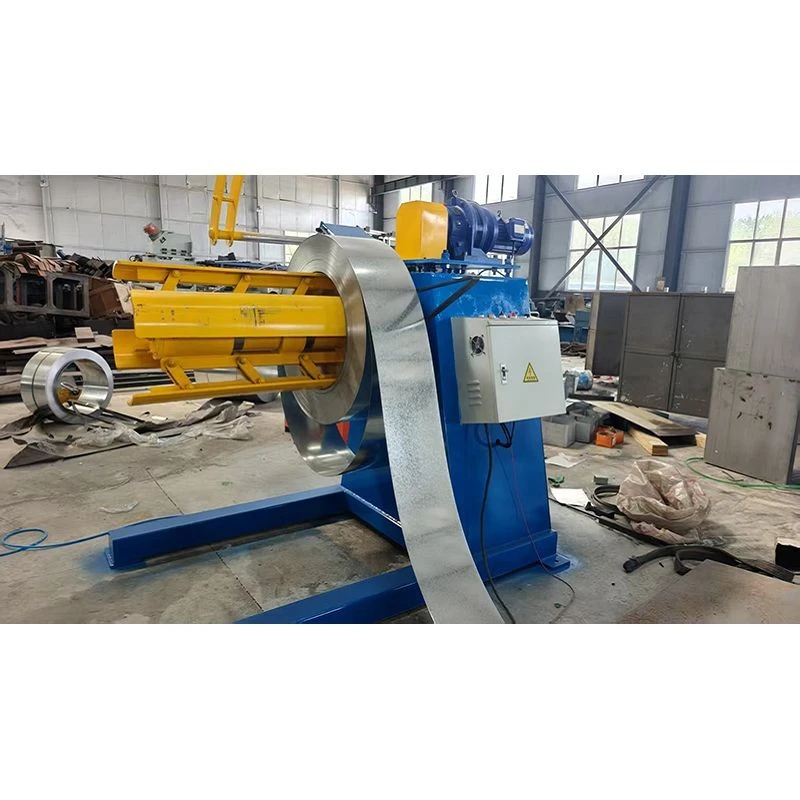
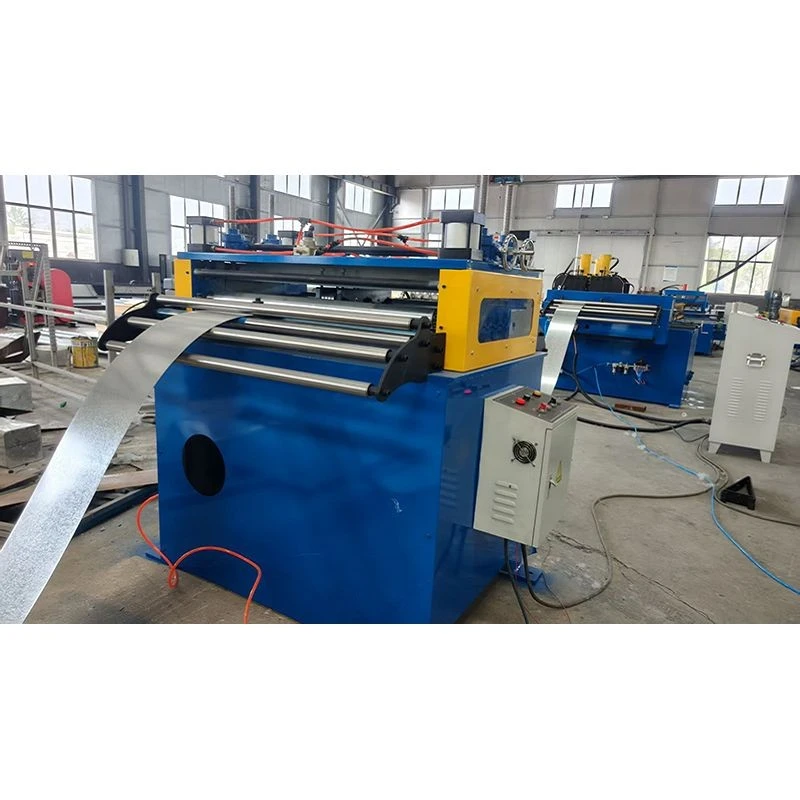
A: This equipment is the core machine of the door panel production line, responsible for the main forming processes such as stamping, cutting, conveying, and bending. The uncoiler, leveler, and electrical control system in the production line are auxiliary equipment, forming a complete production line.
Q: Which is better for cutting: a shearing machine or hydraulic shearing?
A: Shearing machines are suitable for thin plates (0.5-1.5mm), producing smooth, burr-free edges, and the cutting speed matches the production line cycle well. Hydraulic shearing is suitable for thick plates (over 1.5mm), offering greater cutting force but slightly rougher edges. This line uses a shearing machine for cutting thin door panels, eliminating the need for subsequent deburring.
Hot Tags: electrical cabinet door panel manufacturing equipment, China electrical cabinet door panel manufacturing equipment manufacturers, factory


