
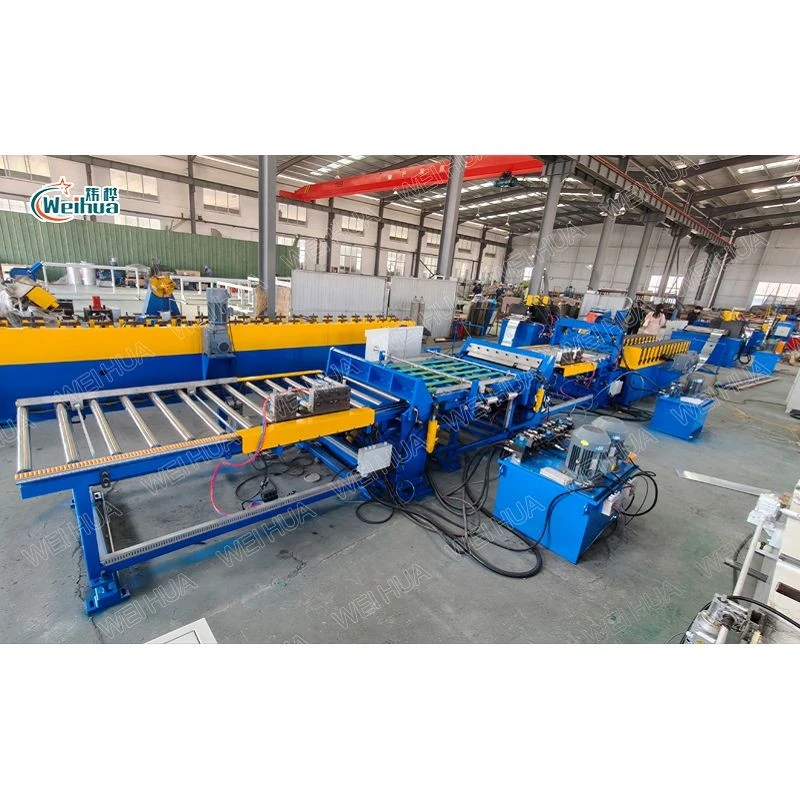
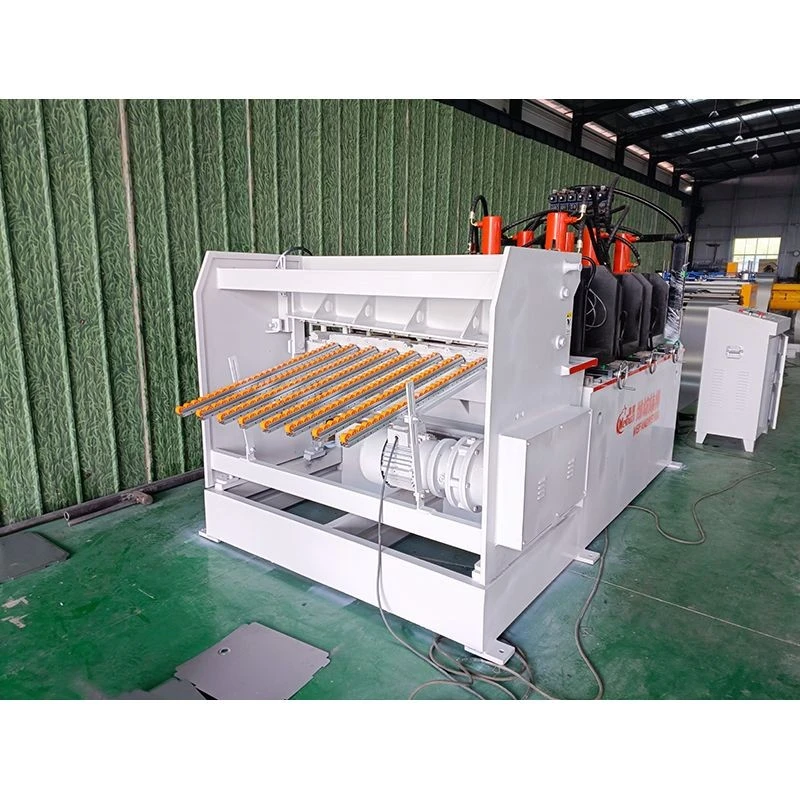
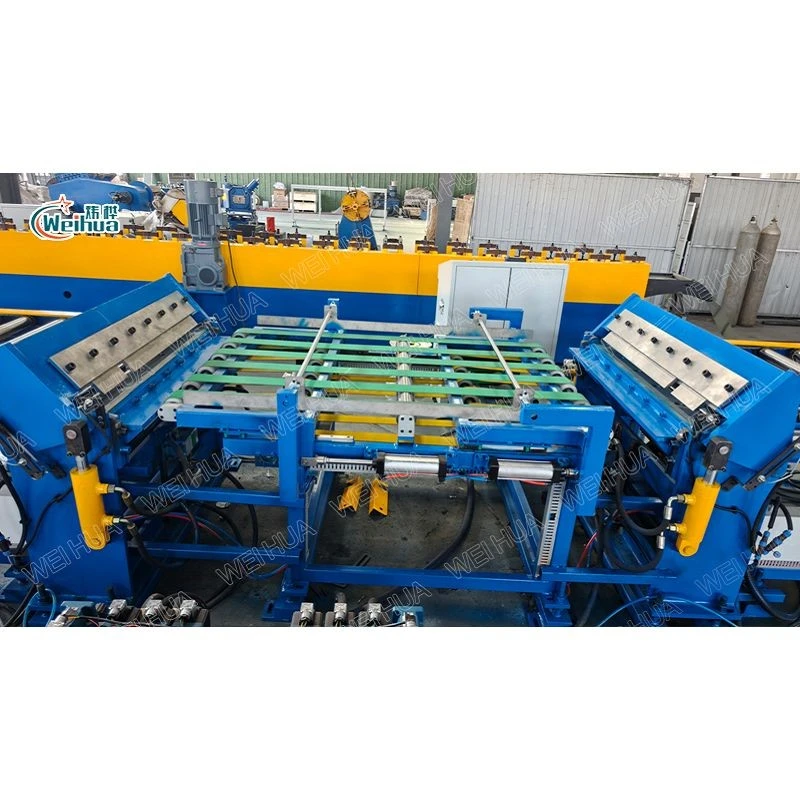
Electrical Cabinet Door Panel Production Line
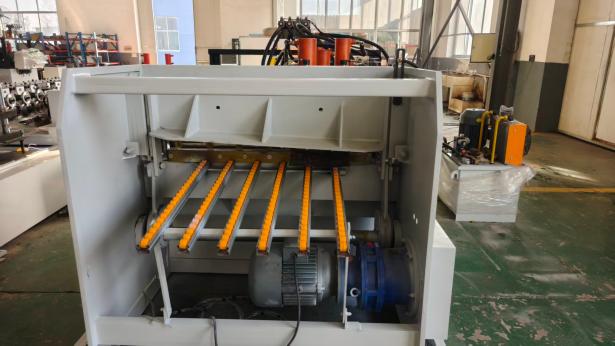
The electrical cabinet door panel production line is an automated equipment specifically designed for one-time molding of electrical cabinet door panels, integrating feeding, punching, cutting, conveying, and bending. As a core component of the cabinet's appearance, the door panel requires pre-set hinge holes and lock holes, and a high degree of surface flatness. This line has a production speed of 0-4 pieces/minute, a power of 30kW, an accuracy of ±0.5mm, and can process plates with a thickness of 0.5-1.5mm and a width of 100-1000mm, suitable for mass production of door panels for high and low voltage switchgear, control cabinets, etc.
Technical Specifications
|
Product Name |
Electrical Cabinet Door Panel Production Line |
|
|
Material Specification |
Q235 |
|
|
Production Speed |
0-4pcs/min |
|
|
Cutting Method |
Shearing Machine |
|
|
Voltage Parameters |
380V/415V, 50Hz, 3-phase |
|
|
Electrical Control |
PLC |
|
|
Drive Motor |
Variable Frequency Motor Drive |
|
|
Strip Thickness |
0.5-1.5mm (Customized according to customer requirements) |
|
|
Strip Width |
100mm-1000mm |
|
|
Roll Material |
Cr12, Quenched HRC58°-62° |
|
|
Hydraulic Oil Type |
46# Hydraulic Oil |
|
|
Gear Oil Type |
18# Gear Oil |
|
|
Total Motor Power |
30KW |
|
|
Cutting Dimension Tolerance |
≤ ±0.5mm (Length ≤ 3000mm) |
|
|
Cutting Die Material |
Cr12MoV |
|
|
Air Source |
0.5m³/Min; Pressure: 0.7MPa |
|

Product Advantages
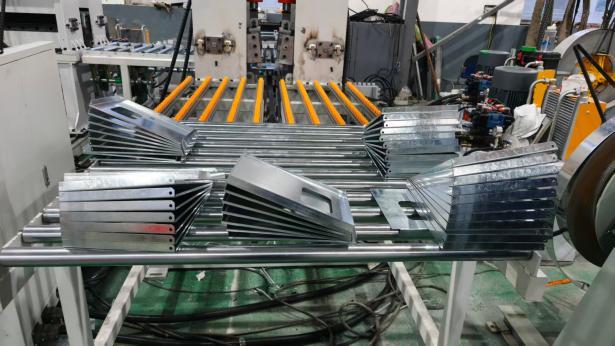
Precise pre-punching of hinge and lock holes eliminates the need for secondary processing during assembly.
The positional accuracy of the hinge mounting holes and lock fixing holes directly affects the smoothness of cabinet door opening and closing and the accuracy of lock alignment. The equipment's stamping system precisely pre-punches hinge and lock holes on the sheet metal according to the customer's door panel assembly drawings. This ensures high hole accuracy and is compatible with both left and right doors. During subsequent assembly, hinges and locks can be directly installed without on-site drilling or hole trimming, significantly improving assembly efficiency, especially suitable for mass production.
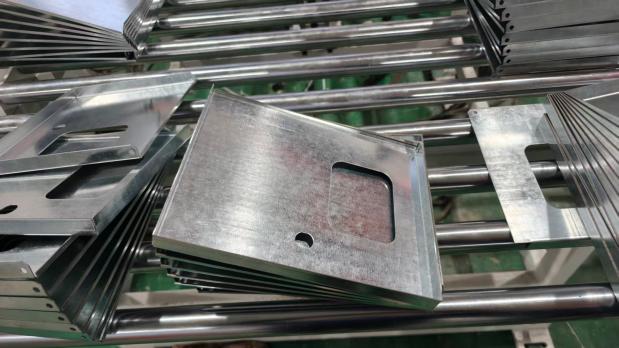
One-time stamping of the observation window opening ensures smooth, burr-free edges.
Electrical cabinet doors with observation windows require rectangular or square windows on the panel. Traditionally, this requires cutting and trimming to remove burrs. The equipment completes the observation window opening processing in one step during the stamping stage. The Cr12MoV die ensures smooth, burr-free cut edges, and the opening size precisely matches standard window accessories, eliminating the need for subsequent cutting, trimming, and deburring, reducing process steps and labor costs.
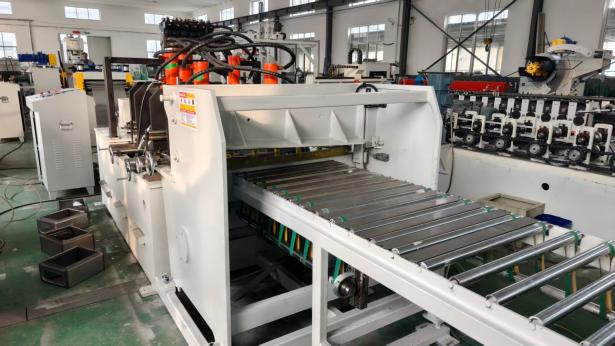
Reinforcing ribs are formed simultaneously using roller pressing, resulting in a smooth, non-distorted panel surface.
Large, thin door panels are prone to "wavy" deformation over long-term use, affecting the cabinet's sealing and appearance. The equipment simultaneously forms longitudinal reinforcing ribs during multiple roller pressing processes. By rationally distributing the position and depth of the reinforcing ribs, the bending rigidity of the door panel is effectively enhanced, while maintaining a smooth, non-distorted surface. This ensures a tight fit between the door panel and the cabinet after bending, smooth opening and closing, and excellent sealing.
Factory photos
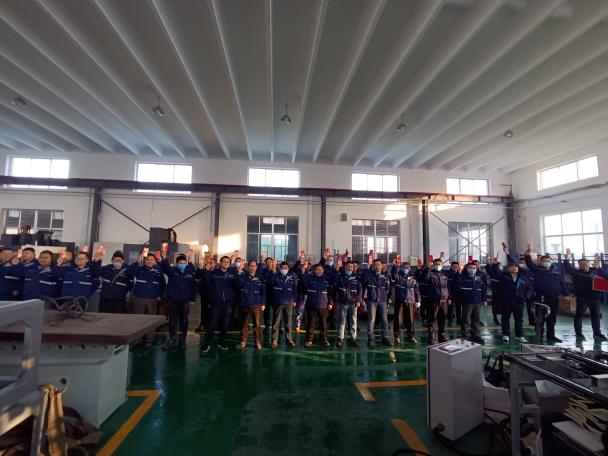
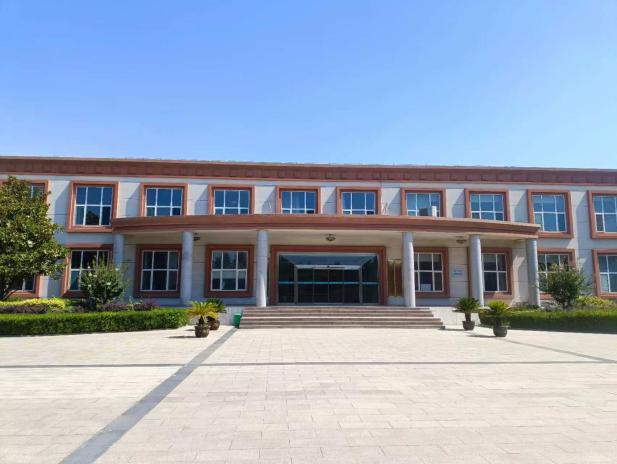
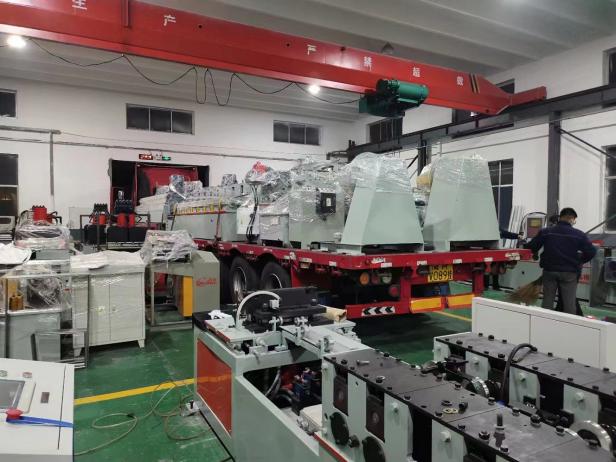
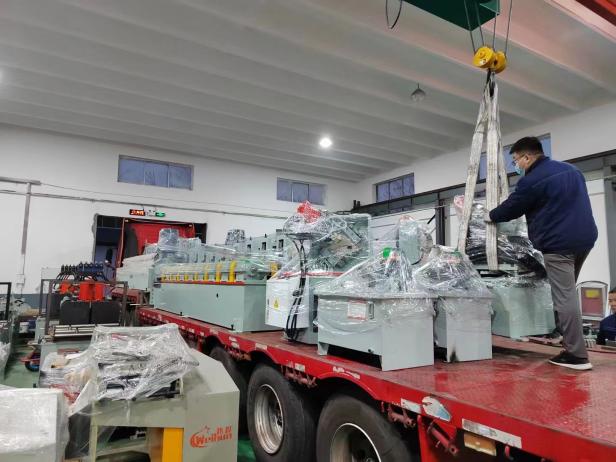
Shipping photos
Customer visit
FAQ
Q: Are you a factory or a trading company?
A: We are a factory located in Weifang, China. It possesses over twenty sets of advanced equipment, including a new precision machining center, NC lathes, CNC wire EDM machines, and a large automotive profile bending test platform. You are welcome to visit our factory at any time.
Q: What's the difference between a fully automatic and semi-automatic door panel production line?
A: A fully automatic line integrates the bending process, continuously producing finished door panels from steel strips. A semi-automatic line only completes the stamping and cutting; manual assistance is required to complete the bending process.
Q: Can you produce door panels with different opening directions?
A: Yes. Left-opening, right-opening, and other directions can be achieved by switching the hole position formula via a PLC program; no mold changes are needed.
Q: Do the four corners of the door panel need to be welded after bending?
A: No welding is required. The four sides are naturally formed by bending. For rounded corner door panels, a rounded bending mold can be configured.
Hot Tags: electrical cabinet door panel production line, China electrical cabinet door panel production line manufacturers, factory


