
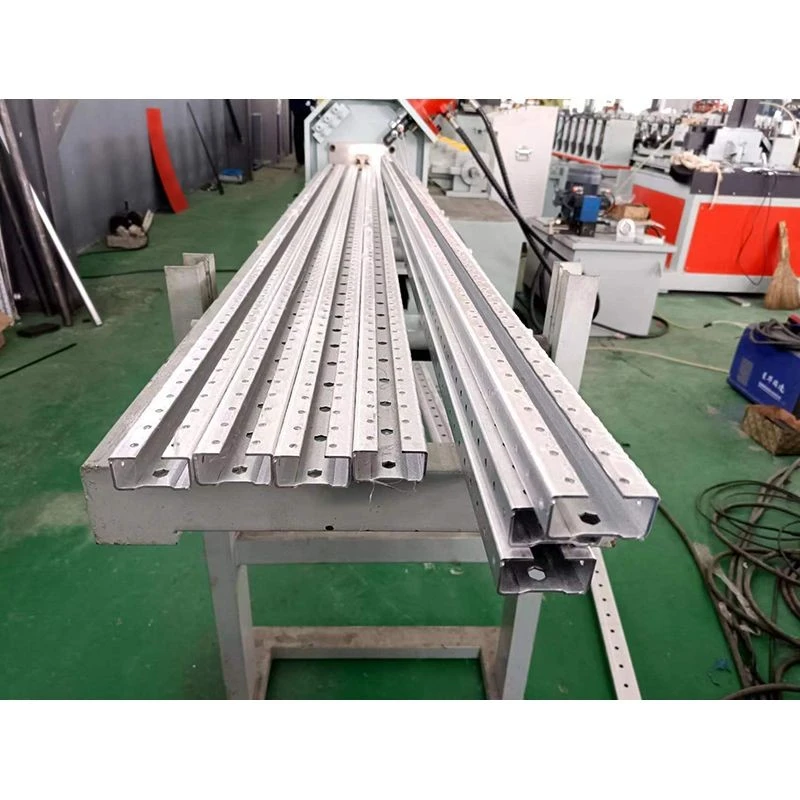
16-Fold Profile Production Line
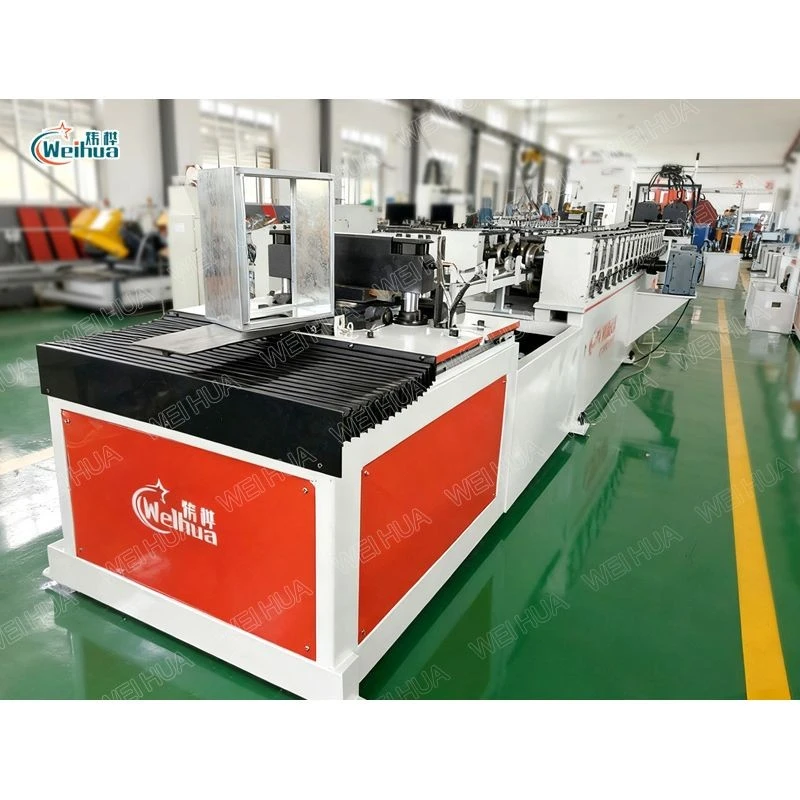
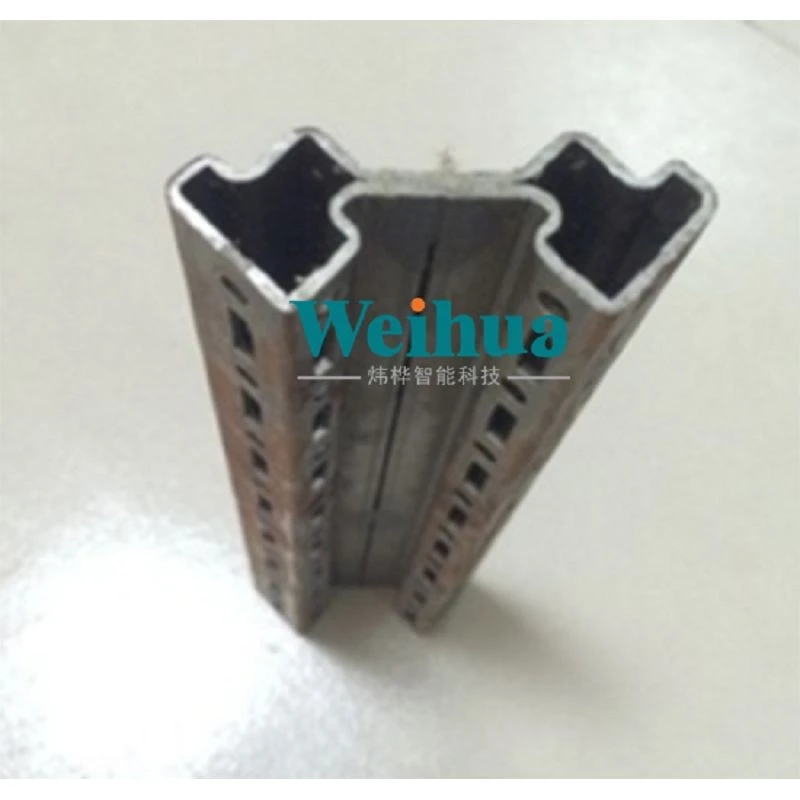
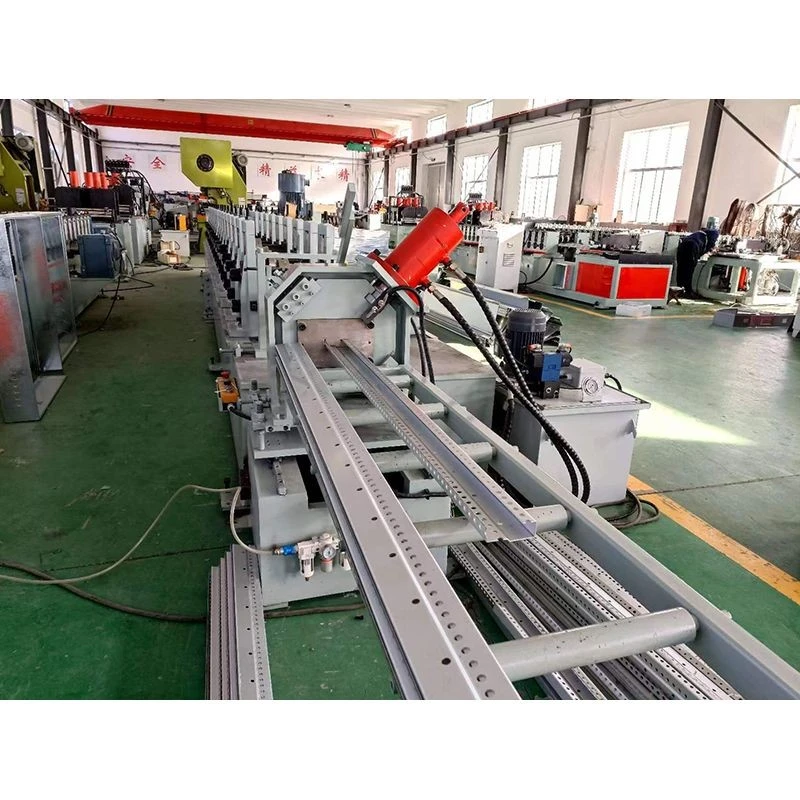
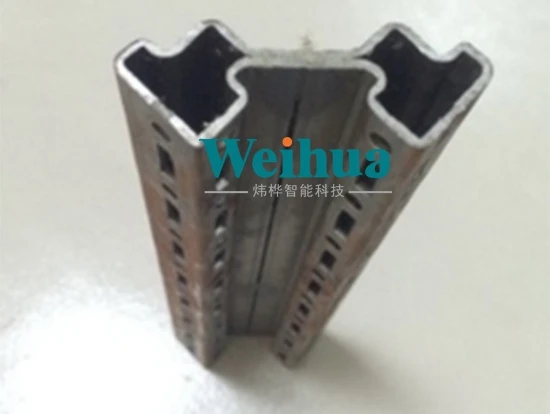
The 16-fold profile production line is an automated equipment specifically designed for processing 16-fold closed-section profiles. These profiles, with their fully enclosed multi-cavity structure formed by 16 bends, are the core frame profiles for heavy-duty cabinets such as Rittal cabinets, PS cabinets, and high-end control cabinets. Their load-bearing capacity and torsional resistance are superior to 9-fold profiles. The equipment integrates uncoiling, leveling, feeding, stamping, forming, and cutting into one unit. It features gantry transmission, Mitsubishi PLC control, a speed of 0-8 m/min, a power of 28 kW, an accuracy of ±0.5 mm, and is suitable for 1.5-2.5 mm thick plates with freely adjustable lengths.

Technical Specifications
|
Product Name |
16-Fold Profile Production Line |
|
Material Specifications |
Q235 cold-rolled strip steel |
|
Material Thickness |
1.5mm/2.5mm (customizable according to user requirements) |
|
Production Speed |
0-8 meters/minute (customizable according to user requirements) |
|
Production Specifications |
Length freely adjustable (customizable) |
|
Voltage Parameters |
380V/415V, 50Hz, 3-phase |
|
Air Source |
0.5m³/min; Pressure: 0.7MPa |
|
Hydraulic Oil Type |
46# Hydraulic Oil |
|
Gear Oil Type |
18# Gear Oil |
|
Roll Material |
Cr12 CNC machined; quenched, hardness reaches HRC58°-60° |
|
Drive Motor |
Variable frequency motor drive |
|
Total Motor Power |
Approximately 28kW (excluding welding parts) |
|
Cutting Die Material |
Cr12MoV |
|
Transmission Mode |
Gantry type + independent transmission gearbox |
|
Cutting Method |
Hydraulic cutting |
|
Cutting Dimension Tolerance |
≤ ±0.5mm (Length ≤ 1000mm) |
|
Operating System |
Touchscreen HMI |
|
Electrical Control |
Mitsubishi PLC Programmable Logic Controller |
|
Legacy Space |
28*3*3 meters (Length × Width × Height) |


Product Advantages
I. Fully Enclosed Multi-Cavity Section Formed in One Step, Achieving Structural Strength Meeting Heavy-Duty Cabinet Requirements
The 16-fold profile features a fully enclosed multi-cavity section, forming multiple closed cavities internally. This significantly improves torsional and bending resistance compared to the 9-fold profile, meeting the frame strength requirements of large, heavy-duty cabinets. The equipment uses multi-pass progressive rolling to form the steel strip into a fully enclosed section in one step, eliminating the need for subsequent welding and removing weak points in the welds.
II. Multi-Pass Bending Stress Released Gradually, Preventing Springback and Corner Cracks
The 16-fold process involves multiple passes and complex deformation, making springback control difficult. The equipment utilizes a refined rolling design to distribute the total deformation across more passes, resulting in smaller deformation per pass and gradual stress release in the sheet metal. This leads to controllable springback and no corner cracks after forming. A finishing roller in the final pass corrects dimensions, ensuring consistency in mass production.
III. Synchronous Pre-punching of Multiple Mounting Holes to Adapt to Complex Internal Component Layouts
All outer surfaces of the 16-fold profile require pre-drilled mounting holes for securing heavy components (high-current switches, copper busbar systems, etc.). The equipment simultaneously punches holes on multiple mounting surfaces of the profile in the stamping section. The hole positions are distributed according to a 25mm module, ensuring a unified positioning reference. The resulting profile exhibits precise hole alignment.
Factory photos
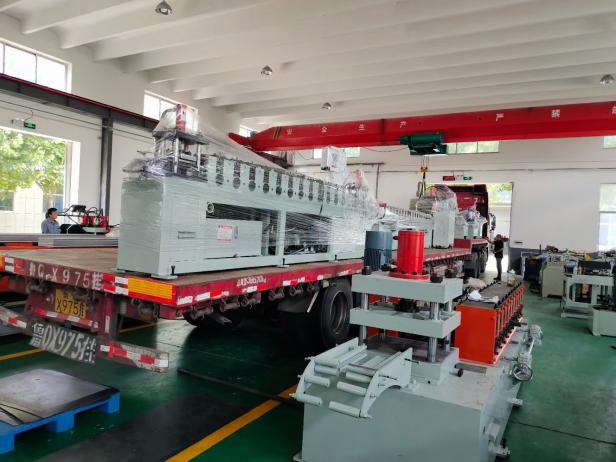
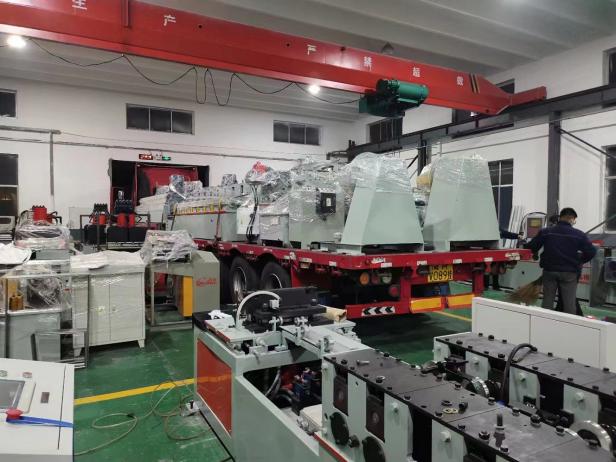
Shipping photos
Customer visit
FAQ
Q: Are you a factory or a trading company?
A: We are a factory located in Weifang, China. It possesses over twenty sets of advanced equipment, including a new precision machining center, NC lathes, CNC wire EDM machines, and a large automotive profile bending test platform. You are welcome to visit our factory at any time.
Q: What are the main differences between 16-fold and 9-fold profiles?
A: 16-fold profiles have a fully enclosed multi-cavity cross-section with multiple closed cavities, resulting in stronger load-bearing and torsional resistance. They are used for large, heavy-duty cabinets. 9-fold profiles have a single-cavity closed cross-section and are used for standard Rittal cabinets. The complexity of their cross-sections and their load-bearing capacity differ.
Q: Can the equipment produce both 16-fold and 9-fold profiles simultaneously?
A: Switching between production is possible, but requires changing the roller set and adjusting parameters. Changeover time is approximately 2-3 hours. Customers can configure two roller sets on the same main unit and switch between them as needed.
Q: Do the mounting holes on the profile surface affect the profile strength?
A: The punching position and diameter are optimized through mechanical calculations and are placed on non-load-bearing surfaces or areas with low stress, so they do not affect the overall load-bearing capacity of the profile. The equipment uses servo control for punching, ensuring precise hole positioning, no burrs, and no additional stress concentration.
Hot Tags: 16-fold profile production line, China 16-fold profile production line manufacturers, factory


